Best Seller
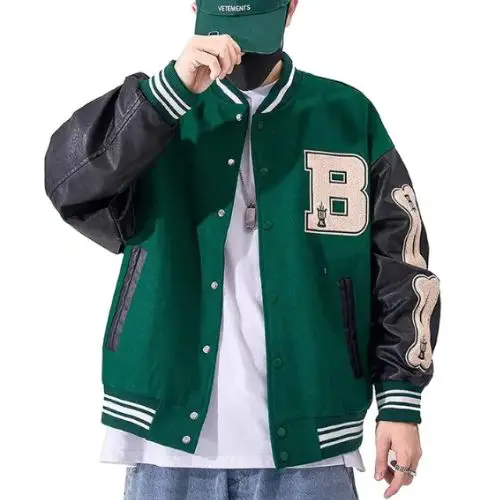
Dark Navy Blue Varsity Jacket
28oz wool blend body with contrast genuine leather sleeves, yarn-dyed striped ribbing, and thermal quilted diamond lining.
28oz WoolCowhide SleevesAQL 2.5
Factory-direct bulk production of classic letterman jackets, baseball shells, and retro collegiate outerwear engineered with premium Melton wool, genuine leather sleeves, and custom 3D chenille patches.
DDP, FOB, and EXW shipment with customs compliance across USA, EU, UK, Canada & Australia.
Flexible production minimums per colorway tailored for independent streetwear labels & distributors.
Sourced from certified mills, paired with top-grain cowhide, lamb nappa, or eco-friendly PU.
3D Chenille patches, felt letters, yarn-dyed 2x2 ribbing, and custom branded metal snaps.
Explore our proven production blocks. Each style features fully customizable body fabrics, sleeve materials, lining densities, ribbing patterns, and patch placement options tailored to your exact brand tech-pack.
28oz wool blend body with contrast genuine leather sleeves, yarn-dyed striped ribbing, and thermal quilted diamond lining.
Black & white traditional collegiate cut with heavy-duty snap fasteners, double welt pockets, and custom neck labels.
High-density custom direct embroidery combined with felt patch detailing for boutique fashion and streetwear labels.
Relaxed oversized fit featuring contrast raglan leather sleeves, interior chest pocket, and high-shine metal snaps.
Lightweight wool-poly body with recycled rPET lining engineered for high-school, college, and university uniform contracts.
Two-tone vintage palette featuring custom-dyed wool body, matte finished leather arms, and 3D chenille letter branding.
Intricate sleeve graphic embroidery with reinforced shoulder seams and heavy 300 GSM cotton-acrylic rib trim.
Combining classic varsity aesthetic with technical flight bomber utility pockets and concealed front brass zipper.
A premium varsity jacket must balance thermal protection, movement flexibility, and structural longevity. We source certified raw materials and employ rigorous stitching standards to ensure your private label garments stand out in the retail environment.
Whether you are launching an exclusive varsity jacket dropshipping range, equipping an collegiate alumni program, or building an autumn/winter streetwear line, our master tailors and merchandisers make custom production seamless.
 Tech Spec
Final Jacket
Varsity jackets feature complex composite assembly—joining thick wool to rigid leather and stretchy ribbing. Our strict inline quality control prevents puckering, alignment errors, and sleeve distortion.
Every wool batch undergoes tensile strength, pilling, and shade-matching tests; leather hides are sorted for uniform thickness and grain texture.
Automated cutting tables maximize fabric yield while computerized Tajima multi-head embroidery machines craft dense chenille patches.
Specialized heavy-duty walking-foot machines join leather sleeves to wool bodies with reinforced double-needle safety stitching.
Every jacket passes through 100% metal/broken-needle detectors, followed by final AQL 2.5 visual inspections before carton sealing.
We offer eco-conscious brands transparent sourcing solutions. From GRS-certified recycled polyester linings to eco-tanned leather and organic cotton ribbing, reduce your environmental footprint without compromising on classic aesthetic.
100% recycled polyester linings produced from post-consumer plastic bottles.
LWG-certified tanneries providing eco-friendly, low-chemical treated hides.
Organic cotton yarns blended with recycled elastane for durable knit trims.
Computerized CAD nesting minimizes wool scrap, recycling excess fibers into felt padding.
All snap buttons, threads, zippers, and linings are tested free from harmful substances.
Fair living wages, safe working environments, and zero forced labor across all facilities.


Sourcing varsity and letterman jackets in bulk requires technical understanding of garment weight, material interaction, and structural integrity. Joining dense 28oz Melton wool to genuine cowhide leather requires heavy-gauge industrial machinery and specialized operator skills. A poorly engineered varsity jacket will sag at the shoulders, pucker along the pocket welts, or suffer color bleeding between the wool body and light-colored leather sleeves. Over the past 16+ years, Oasis Jackets has perfected the varsity pattern block to eliminate these common manufacturing risks.
When designing a varsity jacket range, selecting the appropriate material mix dictates both retail positioning and margin efficiency. For high-end luxury fashion brands, we specify 100% virgin Melton wool combined with full-grain cowhide or supple lamb nappa leather. For collegiate alumni apparel and high-school sports teams, a 28oz wool-polyester blend paired with high-grade eco-PU offers maximum durability, easy maintenance, and competitive price points. For contemporary streetwear labels, we offer relaxed dropped-shoulder cuts crafted from heavyweight 400 GSM fleece or nylon satin bodies with retro contrasting raglan sleeves.
Branding is the soul of a letterman jacket. Oasis Jackets operates in-house Tajima multi-head embroidery and chenille loops machinery. Our digitizing engineers ensure crisp letter boundaries, dense loop fill, and clean felt-backing borders. Whether your tech-pack requires vintage 3D felt letters on the chest, intricate sleeve crests, full-back tackle-twill appliqué, or subtle interior pocket embroidery, every element is sealed and stitch-verified on pre-production samples before bulk cutting begins.
Operating sales and merchandising desks in the United States, United Kingdom, Australia, UAE, Saudi Arabia, Germany, France, Brazil, and Qatar, Oasis Jackets supports global procurement teams through every step of production. We handle tariff documentation, customs classification, GRS/OEKO-TEX compliance certificates, and offer door-to-door (DDP), FOB, or EXW shipping options to streamline your delivery timeline.
Clear answers for apparel buyers, brand founders, and procurement managers regarding bulk varsity jacket manufacturing.
We specify high-performance outerwear fabrics based on your target retail market:
We maintain flexible low MOQs per design and colorway to support growing private label brands. Stock fabric blocks with custom patch application feature lower order thresholds, while custom mill-dyed wool or custom-knitted ribbing patterns have tailored volume requirements.
Yes. Private label manufacturing is our core strength. We produce custom 3D chenille loop patches, felt-backed tackle twill letters, direct sleeve embroidery, custom-branded brass snaps, woven neck tags, care/content labels, and custom polybags.
Sample patterns and digitizing custom patches take 7–10 days. Once the physical pre-production sample is approved, bulk manufacturing takes 25–35 days depending on total order volume and trim complexity.
Yes. Every bulk contract includes a physical sealed pre-production (PP) sample sent directly to your office for approval. Mass production commences only after full written sign-off on fit, stitch quality, and patch accuracy.
Send your tech-pack, reference image, or target price point. Our merchandising team will return a competitive factory quote, material options, and production timeline within 24 hours.