DDP, FOB, or EXW dispatch with consolidated sea and air freight for ski brands.
Flexible Technical MOQ
Start small per technical style and colorway, then scale as sell-through accelerates.
10,000+ Master Blocks
Validated fit patterns for 3L shells, insulated alpine coats, freeride anoraks, and eco skiwear.
Dedicated Merchandiser
One expert contact handling membrane testing, lab dips, tech packs, and AQL 2.5 checks.
Product Catalog & Technical Specifications
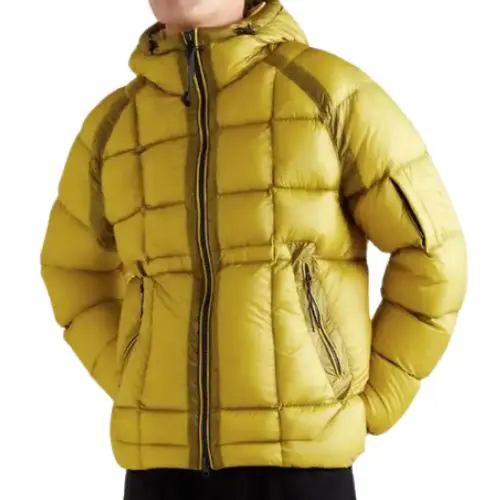
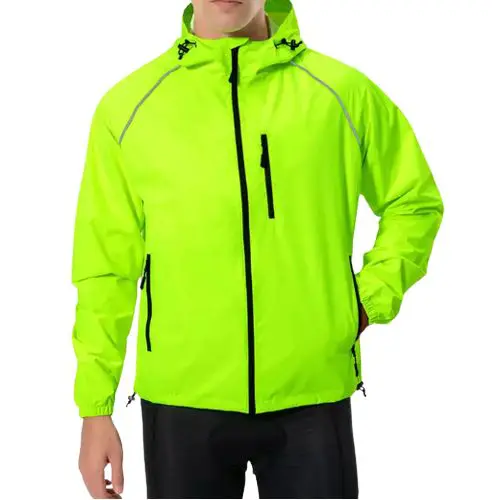
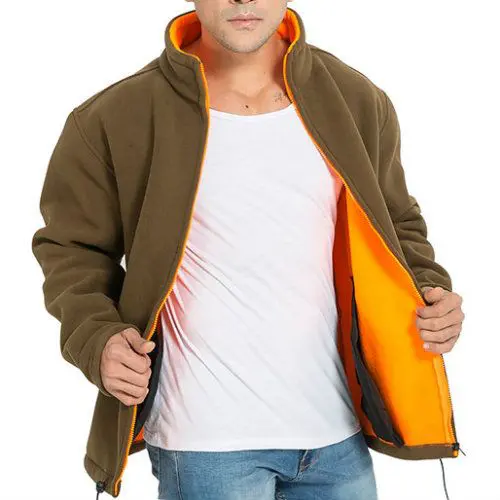
High-Performance Skiing & Snowboarding Jackets for Wholesale
Every item below represents a live production block with graded patterns (XS–5XL), rigorous seam-sealing validations, and lab-tested membrane options. Partner with Oasis Jackets to cut technical development time by up to 40% while preserving maximum margin.
Brands demanding environmental compliance rely on Oasis Jackets for verified green supply chains. Below is our end-to-end GRS-certified process for manufacturing eco-friendly skiing and snowboarding jackets.
rPET Intake
Ocean-bound plastic bottles and ghost nets are recovered and cataloged by polymer batch.
Yarn Extrusion
Recycled chips are spun into high-tenacity 75D/150D hydrophobic polyester filament yarn.
Ripstop Weaving
Yarn is woven on high-speed looms with micro-ripstop grids to prevent snow tearing.
Membrane Lamination
Hydrophilic bio-based polyurethane membranes are hot-laminated for 20K–30K waterproofness.
PFC-Free DWR
Fluorine-free DWR coatings are applied, meeting strict European REACH and California AB 1817 regulations.
GRS TC Issuance
Every shipment is delivered with Transaction Certificates (TC) validating true recycled origin.
OEM/ODM Technical Precision
Transforming Conceptual Tech Packs into Sealed Alpine Outerwear
Whether you bring a complete technical spec sheet, a 3D CAD rendering, or a target market price point, our Beverly Hills engineering desk and master pattern makers reverse-engineer seam lines, membrane weights, zipper tolerances, and insulation density. We eliminate production risk before the first fabric roll is cut.
3D CLO digital pattern grading and pressure-mapping for snowboarding movement
Direct fabric sourcing: ePTFE/TPU membranes, Cordura®, PrimaLoft®, and YKK AquaGuard®
Live video fit testing and cold-chamber thermal testing validation
Sealed Pre-Production (PP) golden sample serving as the immutable audit baseline
Controlled Technical Production Stages for Skiwear
Winter sports outerwear faces zero tolerance for manufacturing flaws. A single leaking seam or weak zipper slider compromises safety on the mountain. Here is how our four-stage quality assurance protocol guarantees performance.
Stage 01
Membrane & Dye Lot Testing
Hydrostatic head (ISO 811) testing up to 30,000mm, MVTR breathability check, and spectro-photometer color matching for consistent pan-seasonal dye lots.
Stage 02
Laser Cutting & Hot-Melt Seam Taping
Precision computer-controlled laser cutting followed by automated hot-air seam-sealing machinery applying 3-layer PU tape at 220°C across all stitch lines.
Stage 03
Thermal Baffling & Hardware Assembly
Down-proof stitch integrity checks, ultrasonic bonding of baffle chambers, and reinforced bartacking at key stress points like snow-skirt snaps and pit zips.
Stage 04
Hydrostatic Centrifuge & AQL 2.5 Audit
Continuous water-column pressure testing of random sample garments, metal detection, ratio packing, and pre-shipment photographic compliance reports.
01
Fabric & Membrane Intake
100% roll inspection under 4-point system; membrane peeling force audit.
02
Hardware Pull-Test
Zipper pullers and snap buttons tested to 100N pull force resistance.
03
Inline Seam Testing
Hourly hydrostatic leak testing of taped seams at 0.35 bar for 3 minutes.
04
Final AQL 2.5 Sampling
Rigorous final inspection covering sizing, waterproofing, symmetry, and trim placement.
Enterprise Reliability
Why Premier Winter Sports Brands Trust Oasis Jackets
From established European alpine heritage labels to fast-growing North American freeride direct-to-consumer brands, apparel buyers choose us because we merge technical mastery with flexible financial terms.
01 · Turnkey Snow Sports Portfolio
Single-source solution for 3L technical shells, freeride insulated jackets, softshell ski pants, backcountry bibs, and mid-layer grid fleeces. Consolidate your winter buying with one trusted manufacturer.
02 · Low MOQ for Accelerated Market Testing
Don't lock capital in unproven inventory. Launch custom skiwear collections with flexible minimums per style/colorway, utilizing our pre-certified membrane shells and stock trim programs.
03 · Component-Level Private Label Customization
Custom-dyed technical shells to Pantone, branded heat-transfer seam tape, laser-etched silicone badges, custom waterproof zippers, FTC/EU compliant care labels, and branded recycled packaging.
04 · Transparent Open-Costing Structure
We break down fabric yield, membrane lamination costs, seam sealing SAM (Standard Allowed Minutes), trim expenditures, and freight options—ensuring your retail margin is protected before production begins.
Production Capacity
Global Manufacturing Footprint
Experience16+ Years
Sales Offices7 Countries
Production Units9 Countries
Shipping To55 Countries
Developed Styles10,000+
Clients Served5,000+
Merchandising Team100+ People
Factory Workforce2,000+ People
Enterprise Trust
Institutional Clients, Global Brands & Winter Sports Partners
Certifications & Audits
International Quality & Sustainability Audits
Global Operations
Localized B2B Support Across 7 Key Continents
Sourcing complex technical outerwear across borders requires accountable regional management. Our international hubs handle technical costing, customs clearance paperwork, lab dip approvals, and direct account management.
United States · HQ
8730 Wilshire Blvd, Penthouse, Beverly Hills, Los Angeles, CA 90210
Engineering High-Performance Skiing & Snowboarding Jackets: A Technical Procurement Masterclass
In the competitive landscape of winter sports outerwear, manufacturing high-performance Skiing Snowboarding Jackets is an intricate engineering challenge. Unlike lifestyle outerwear, technical snow sports garments must deliver unyielding protection against extreme alpine sub-zero temperatures, gale-force winds, driving precipitation, and severe mechanical friction. For global apparel brands, retail chains, and outdoor equipment distributors, sourcing ski and snowboard jackets requires a deep understanding of membrane physics, hydrostatic head tolerances, seam sealing chemistry, ergonomic patterning, and global compliance regulations.
At Oasis Jackets, operating under the global umbrella of Dioz Group, we have spent over 16 years refining OEM and ODM manufacturing pipelines across 9 production countries. Our engineering philosophy centers on mitigating brand risk through rigorous pre-production testing, open-cost transparency, and component-level technical control. This technical guide outlines how global buyers can navigate the future of skiwear manufacturing, optimize sourcing intent, and build high-margin winter collections.
Hydrostatic Resistance
10,000mm – 30,000mm H₂O
Seam Sealing Standard
3L Hot-Melt PU Tape @ 0.35 bar
Inspection Protocol
Inline & Final AQL 2.5 Audit
Technical Architecture: Deconstructing the Modern Ski & Snowboard Jacket
To create a commercially successful technical ski or snowboard jacket, sourcing directors must evaluate the interaction between three fundamental structural layers: the outer face fabric, the waterproof-breathable membrane, and the internal lining or thermal insulation matrix.
1. Outer Shell Fabrics & Abrasion Resistance
The face fabric acts as the primary barrier against environmental elements and mechanical wear. For alpine skiing, where aerodynamic speed and friction against icy packed snow dominate, high-density 75D to 150D mechanical stretch polyester or nylon-6,6 weaves are preferred. Snowboarding garments, by contrast, demand elevated abrasion resistance due to frequent contact with board edges, terrain park features, and snow seating. We specify micro-ripstop nylon reinforced with 500D Cordura® panels across seat, shoulder, and forearm zones to prevent premature tearing.
2. Waterproof & Breathable Membrane Technologies (ePTFE vs. TPU)
The functional engine of any skiing and snowboarding jacket is its internal membrane laminate. We engineer custom outerwear utilizing two distinct membrane chemistries depending on brand positioning:
Expanded Polytetrafluoroethylene (ePTFE): Delivers elite performance ratings exceeding 28,000mm hydrostatic head and breathability under 6 RET (Resistance to Evaporative Heat Transfer). Ideal for backcountry tourers and extreme alpine environments where vapor management is critical.
Hydrophilic Polyurethane (TPU) Laminates: Provides robust 10,000mm to 20,000mm hydrostatic protection with excellent stretch elasticity and cost-effective yield. Perfect for commercial resort skiing and high-volume retail lines.
3. Thermal Mapping & Insulation Systems
Over-insulating a ski jacket leads to moisture buildup during intense physical activity, causing post-exertion hypothermia. Our pattern room implements thermal-mapping technology: placing 100GSM to 120GSM PrimaLoft® Gold or GRS-certified recycled polyfill around core chest and back panels, while reducing sleeve and underarm zones to 60GSM or 80GSM. For ultra-light powder jackets, baffle-welded 700-fill-power down with hydrophobic treatment provides unmatched warmth-to-weight ratios.
Future Procurement Trends in Ski & Snowboard Outerwear (2025–2030)
The winter sports apparel industry is undergoing unprecedented structural shifts driven by environmental legislation, consumer behavior, and material science innovations. Sourcing managers must align their manufacturing pipelines with these emerging global trends to maintain competitive edge:
1. The Mandatory Shift to PFAS-Free / PFC-Free DWR Coatings
Regulatory crackdowns across Europe (REACH standards) and North America (including California's AB 1817 banning intentionally added PFAS in textiles by 2025) have made traditional C8 and C6 fluorocarbon water-repellent treatments obsolete. Oasis Jackets has pioneered bio-based, fluorine-free DWR finishes derived from plant waxes and non-toxic silicone polymers. Our PFC-free coatings maintain a 90/10 water repellency rating even after 20 domestic wash cycles, satisfying both regulatory mandates and eco-conscious consumer intent.
2. Circular Monomaterial Design & Digital Product Passports (DPP)
Future-proof outerwear must be designed for end-of-life recyclability. Traditional jackets blending nylon shells, polyurethane membranes, and polyester linings cannot be mechanically recycled without expensive separation. We are leading the transition toward 100% Polyester Monomaterial Garments—combining rPET face fabric, rPET membrane, rPET insulation, and rPET sewing thread. Furthermore, we assist brands in integrating QR-coded Digital Product Passports (DPP) inside internal care pockets, allowing consumers and recyclers to scan fabric composition and supply chain origin instantly.
Safety and tech-integration are transitioning from luxury add-ons to standard commercial expectations. Our manufacturing lines seamlessly incorporate ultrasonically welded RECCO® Rescue Reflectors into sleeves and hoods, requiring no batteries while enabling radar location by search teams. Additionally, we produce active-heating skiwear incorporating flexible carbon-nanotube heating panels powered by slim lithium power banks, controllable via Bluetooth smartphone apps for cold-chairlift comfort.
Geopolitical friction, tariff volatility, and climate-induced shipping delays have exposed the danger of relying on a single manufacturing hub. Operating facilities across 9 countries allows Oasis Jackets to offer strategic geographic diversification. US brands can utilize duty-advantageous production nodes, while European clients benefit from expedited Mediterranean shipping corridors, safeguarding seasonal launch deadlines.
Direct OEM/ODM Procurement Desk
Looking to launch a custom 10K-30K skiing or snowboarding jacket line? Consult with our senior technical merchandisers for instant fabric costings, lab dip timelines, and minimum order structures.
Comprehensive Technical Procurement FAQ for Global Buyers
Below are real-world technical and operational queries submitted by global procurement teams, importers, and private label founders searching for reliable skiwear manufacturing partners.
Technical Sourcing Intelligence
Frequently Asked Sourcing Questions
Clear, authoritative technical answers to help you navigate winter sports apparel manufacturing, quality control, and international logistics.
How do you verify hydrostatic head and MVTR breathability ratings before bulk ski jacket production?
Hydrostatic pressure and breathability testing are conducted on both raw fabric rolls and post-production seam lines:
Hydrostatic Head Testing (ISO 811 / AATCC 127): Fabric samples are subjected to a rising column of water pressure. For 20,000mm ratings, the fabric must withstand 2.0 bar of water pressure before a third drop penetrates the membrane surface.
Moisture Vapor Transmission Rate (JIS L 1099 B1 / ASTM E96): Measures the grams of water vapor escaping through a square meter of fabric over 24 hours. Our pro 3L shells achieve up to 25,000g/m²/24h.
Third-Party Validation: Certified lab reports from SGS, Intertek, or Bureau Veritas are provided with sealed pre-production samples prior to bulk cutting approval.
What is the minimum order quantity (MOQ) for custom private label snowboarding and skiing jackets?
We structure MOQs to support both established brands and scaling independent labels. For programs utilizing our pre-certified stock technical fabrics and available membrane shells, our MOQ starts at 100 to 300 pieces per style/colorway. For fully customized mill-dyed pantone fabrics, custom jacquard internal linings, or engineered print placements, mill minimums generally require 500 to 1,000 units. We allow size splits from XS through 5XL within the minimum quantity block.
How does Oasis Jackets solve seam sealing tape failure during heavy winter use?
Seam tape delamination is the primary cause of skiwear failure. We prevent tape breakdown by: (1) matching the melt-point chemistry of the 3-layer PU hot-melt tape exactly to the internal membrane coating, (2) using computer-calibrated hot-air sealing machines maintaining precise temperature (210°C–230°C) and pressure rollers, and (3) testing every seam line under continuous 0.35 bar hydrostatic water pressure for 3 minutes during hourly inline QC audits.
What certifications do your manufacturing facilities hold for ethical and eco-friendly ski jacket manufacturing?
Our primary production units and tier-1 fabric suppliers maintain full international accreditation including: Global Recycled Standard (GRS), Recycled Claim Standard (RCS), OEKO-TEX Standard 100 Class I, GOTS organic compliance, amfori BSCI social audits, Higg Index FEM environmental monitoring, and IDFL certification for responsibly harvested non-live-plucked down. We issue official Transaction Certificates (TC) per shipment.
Can you integrate complex technical trims like RECCO® reflectors and YKK AquaGuard® zippers?
Yes. Our pattern room and production lines are equipped for advanced component assembly. We perform ultrasonic pocket welding, laser-cut bonded zipper tracks, automated setting of YKK AquaGuard® water-repellent zips, magnetic pocket flap closures, internal stretch LYCRA® cuff gaiters, 3D adjustable helmet-compatible hood cordage, and seamless integration of RECCO® rescue transponders into sleeve or hood brim positions.
What is the typical production timeline for prototype sampling and bulk container delivery?
Our standard manufacturing schedule operates as follows: 7 to 12 working days for digital pattern creation, tech-pack refinement, and initial proto sampling; 5 to 7 days for lab-dip color matching and trim approvals; and 30 to 45 days for bulk production once the Pre-Production (PP) golden sample is sealed. Air freight shipping takes 5–9 days, while consolidated sea freight takes 20–40 days depending on port of destination.
How do you ensure color fastness, cold-crack resistance, and hardware durability in sub-zero alpine conditions?
All technical fabrics, zippers, drawcords, and TPU badges undergo cold-chamber freeze testing down to -30°C to guarantee materials do not become brittle or snap under sub-zero impact. Fabrics undergo ISO 105-B02 light fastness testing (rating 4-5) and ISO 105-C06 wash fastness checks to ensure vibrant alpine colorways do not bleed or fade from UV snow reflection.
Do you assist startup private label brands with tech packs and regulatory customs compliance?
Absolutely. A substantial portion of our client base consists of growing direct-to-consumer outerwear brands. Our Beverly Hills design desk helps translate rough sketches into production-ready tech packs, provides advice on size grading for target US/EU/APAC demographics, and ensures your inner care labels comply with US FTC textile regulations, EU REACH laws, and local fiber composition disclosure rules.
The Oasis Advantage
Partnering with a Global Outerwear Powerhouse
Choosing the right manufacturing partner for your Skiing Snowboarding Jackets line is the single most critical decision in determining your brand's seasonal profitability and market reputation. When you partner with Oasis Jackets, you gain direct access to a world-class infrastructure that bridges high-fashion aesthetic design with heavy-duty technical performance engineering.
With executive headquarters located at 8730 Wilshire Blvd, Beverly Hills, and dedicated sales, compliance, and merchandising desks in the United Kingdom, United Arab Emirates, Saudi Arabia, Australia, Brazil, Germany, France, and Qatar, we offer 24/7 client support across all major time zones. Our global production footprint spans 9 certified countries, allowing us to optimize tariff structures, streamline shipping routes, and safeguard your supply chain against regional disruptions.
Start Your Custom Ski & Snowboard Outerwear Line Today
Whether you are planning a high-volume commercial ski resort uniform order, expanding an established winter activewear collection, or launching an innovative private label freeride snowboard brand, Oasis Jackets is prepared to execute your vision with zero compromise on quality.
Send us your flat sketches, competitor sample garments, or conceptual tech packs. Our merchandising engineering team will deliver a comprehensive proposal including material alternatives, hydrostatic performance options, transparent costing breakdowns, and a realistic production timeline within 24 hours.