Custom Varsity Jackets: Technical Blueprint & Global Sourcing Standards
Engineered for apparel brands, streetwear labels, and global distributors. 24oz virgin Melton wool, top-grain leather, custom 3D chenille embroidery, low MOQs, and factory-direct control across 9 production countries.
Direct access to apparel engineers for tech-pack creation, pattern grading, marker efficiency, and cost optimization.
Product Engineering & Recommendations
Custom Varsity Jacket Lineup for Private Labels & Bulk Buyers
From traditional Ivy League heritage designs to oversized streetwear silhouettes, our varsity jacket production blocks are pre-graded from XS to 5XL. Each category represents a battle-tested blueprint ready for immediate customization and high-margin retail positioning.
Heritage Heavyweight
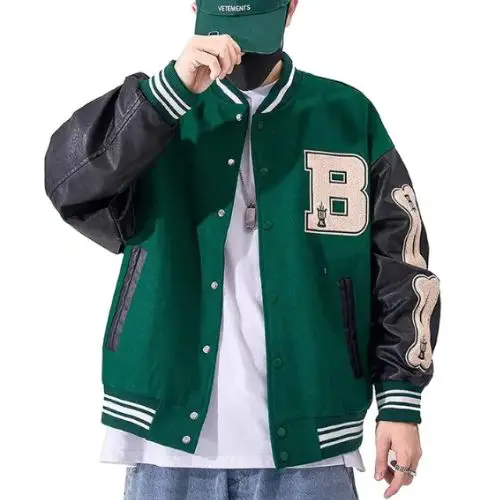
Classic Heavyweight Letterman
24oz–28oz Melton wool body with genuine drum-dyed cowhide sleeves. Diamond quilted satin lining, heavy snap closures, and custom chenille chest lettering.
How Recycled & Certified Custom Varsity Jackets Are Manufactured
To eliminate greenwashing and ensure strict compliance with global import regulations (such as EU Digital Product Passports and US FTC rules), every material stage in our varsity jacket supply chain is independently audited and documented.
Raw Intake
Sorting post-consumer PET bottles and pre-consumer post-industrial wool scraps for re-spinning.
Polymization
Thermal extrusion transforms recovered textiles into high-tenacity rPET yarn and recycled wool fibres.
Carton drop testing, needle detection, and GRS/OEKO-TEX transaction certificate release per batch.
Tech-Pack Engineering
From 2D Vector Design to Production-Sealed Varsity Sample
Procuring custom varsity jackets requires absolute precision in trim matching, leather thickness, and chenille patch density. Our CAD pattern team translates flat sketches into production-ready tech packs within 48 hours, optimizing seam construction and fabric yield before cutting bulk cloth.
24oz Melton Wool vs Recycled Wool-Blend options with lab dips
0.9mm-1.2mm Drum-Dyed Cowhide, Lambskin, or Bio-PU sleeve selection
Computerized 3D Chenille & Felt Patch digitizing with zero distortion
Custom 2x2 Yarn-Dyed Ribbing with Spandex recovery to prevent sag
Unlike standard garments, custom varsity jackets combine heavy woven wool, thick leather hides, layered embroidery, and elasticized ribbing. Each step must adhere to rigorous quality checkpoints to guarantee durability and fit perfection.
Stage 01
Wool & Leather Inspection
Raw wool rolls undergo 4-point inspection for density and pill resistance; leather hides are sorted by thickness (1.1mm±0.1mm) and grain consistency.
Stage 02
Precision CAD Panel Cutting
Computer-controlled laser cutters shape heavy Melton wool and leather sleeve panels, ensuring sub-millimeter seam allowance accuracy.
Stage 03
Chenille Patch & Assembly
Multi-thread embroidery heads stitch felt-backed chenille badges directly onto panels prior to heavy-duty leather sleeve insertion and double-needle joining.
Stage 04
Hardware Audit & AQL 2.5
Every snap closure undergoes pull-force testing (>120N); jackets pass metal detection, thread trimming, steam molding, and final AQL 2.5 audit.
01
Fabric & Leather Audit
100% inspection of hides and wool lots prior to pattern layout.
02
Emblem Precision
Chenille stitch density checked for fluffiness, border tightness, and backing strength.
03
Structural Seams
Reinforced double-stitching on armholes and pocket welts to prevent sleeve tearing.
04
Sealed Box QC
Barcoded ratio-packing, anti-humidity gel inserts, and drop-tested export cartons.
Enterprise Manufacturing Capability
Why Sourcing Directors Choose Oasis Jackets for Custom Varsity Orders
With over 16 years of specialized outerwear production, Oasis Jackets operates as a global supply-chain partner for elite brands, collegiate retail networks, and corporate uniform buyers across 55+ countries.
01 · Industry-Leading Material Engineering
We house an extensive mill network supplying 100% Virgin Melton Wool, recycled wool blends, top-grain cowhide, drum-dyed lambskin, and eco-friendly bio-based leather alternatives. Every material is pre-tested for colorfastness, crocking, and tear resistance.
02 · Flexible MOQs Built for Scalability
Avoid high inventory risks. Our flexible order volumes allow fashion startups and established labels alike to launch seasonal custom varsity capsule collections without over-extending working capital.
03 · Complete Private Label Branding Solutions
From custom woven neck labels, FTC/EU care labels, and branded snap caps to laser-engraved zipper pulls, custom polybags, and retail hangtags — we deliver a 100% ready-to-sell product with zero factory marks.
04 · Transparent Open-Costing Structure
We provide full breakdown visibility across fabric yield, leather square-footage consumption, trim costs, embroidery stitch counts, SAM (Standard Allowed Minutes), and international shipping charges.
Production Capacity & Infrastructure
Global Sourcing Scale at a Glance
Industry History16+ Years
Global Regional Hubs7 Countries
Certified Factories9 Countries
Active Export Markets55+ Nations
Master Patterns10,000+ Blocks
B2B Apparel Clients5,000+ Brands
Merchandising Staff100+ Experts
Factory Floor Workforce2,000+ Personnel
Enterprise Trust
Trusted by Global Corporations, Sports Properties & Government Agencies
International Merchandising Desk & Regional Account Managers
Managing overseas outerwear manufacturing is seamless with local account directors in your time zone. Our regional offices oversee sampling, compliance paperwork, customs brokerage, and logistics.
United States · Global HQ
8730 Wilshire Blvd, Penthouse, Beverly Hills, Los Angeles, CA 90210
The Comprehensive B2B Blueprint for Custom Varsity Jackets Sourcing
In the competitive global outerwear market, procuring custom varsity jackets requires far more than picking a template from a supplier catalog. The classic varsity letterman jacket—originally rooted in American collegiate athletics—has evolved into a high-margin centerpiece for luxury streetwear brands, lifestyle retail labels, sports franchises, and corporate merchandise programs. However, because a varsity jacket is a complex hybrid garment combining heavy woven wool, thick leather or synthetic hides, dense multi-layered chenille embroidery, yarn-dyed elastane ribbing, and technical snap closures, structural failure at any single component can ruin an entire production run.
As a specialized manufacturer with over 16 years of OEM/ODM outerwear experience, Oasis Jackets engineers custom varsity jackets from the fiber level up. This technical guide outlines the material benchmarks, manufacturing workflows, quality assurance protocols, and future market trends that global procurement directors and private label founders must understand to maximize gross margins while protecting brand integrity.
Wool Specification
24oz–28oz Virgin Melton
Leather Tensile Strength
> 220 N/mm² (ISO 3376)
Embroidery Density
12,000+ stitches/100cm²
1. Anatomy of an Enterprise-Grade Custom Varsity Jacket
To understand manufacturing costs and quality differentials, buyers must evaluate the four key physical pillars of a custom varsity jacket:
A. The Body: Melton Wool vs. Recycled Fleece Blends
The traditional foundation of any premium letterman jacket is Melton wool. Named after Melton Mowbray in England, authentic Melton fabric undergoes a rigorous fulling process—where heat, moisture, and mechanical agitation shrink and compact the woven wool fibers into a dense, smooth, wind-proof barrier. At Oasis Jackets, we offer three distinct wool classes:
24oz to 28oz Virgin Melton Wool (80% Wool / 20% Nylon): The gold standard for premium retail and heritage varsity jackets. Nylon is blended to increase tear strength and color retention while preserving natural wool breathability.
Recycled Wool-Poly Blend (GRS Certified): Engineered from post-industrial garment scraps. Reduces carbon footprint by 45% while delivering an ultra-soft handfeel suitable for climate-conscious fashion labels.
Lightweight Wool Blend (16oz–18oz): Optimized for spring/summer transitional capsules or warmer tropical climates in Southern Europe, the Middle East, and APAC.
B. The Sleeves: Genuine Hides vs. Advanced Bio-Based PU
Sleeve material selection directly dictates garment drape, break-in period, and final retail price points:
Drum-Dyed Top-Grain Cowhide (1.0mm – 1.2mm): Rugged, heavy, and extremely durable. Ideal for traditional heritage letterman jackets requiring structured sleeve shape retention.
Lamb Nappa Leather (0.8mm – 0.9mm): Supple, buttery handfeel with zero break-in time required. Preferred by high-end luxury fashion brands targeting premium urban clientele.
Bio-Based & Solvent-Free Synthetic Leather: Next-generation PU engineered without DMF or phthalates, offering high flex-crack resistance (tested up to 50,000 cycles on the Flexometer).
C. Embellishments: 3D Chenille Patches & Direct Embroidery
Emblems are the visual soul of a varsity jacket. Inferior suppliers use low-density acrylic yarn that pills and unravels after minimal wear. Oasis Jackets utilizes automated Tajima multi-head embroidery systems to execute high-density chenille patches onto 100% heavy wool felt backings. We engineer chenille loop heights between 4mm and 8mm, crisp chain-stitch borders, and heat-activated backing films to ensure patches remain perfectly flat and permanently fused prior to perimeter stitching.
D. Trim Hardware & Ergonomic Ribbing
A varsity jacket’s ribbing (collar, cuffs, and hem) must withstand hundreds of stretch cycles without losing shape. We spin 2x2 heavy-gauge acrylic yarn with 5% elastane threading to guarantee shape recovery. Snap closures are spec’d in heavy-duty solid brass or anti-rust stainless steel, pass 120 Newton pull-tests, and can be customized with matte, polished, or rubberized branded caps.
2. Future Sourcing Trends in the Custom Varsity Jacket Market (2025–2030)
As search behavior on AI search engines (like SearchGPT, Perplexity, and Gemini) shifts toward sustainable production, supply chain transparency, and multi-functional outerwear, B2B buyers must align their tech packs with emerging macro trends:
Trend 1: The Transition to PFC-Free Water Repellency
Historically, wool bodies were left untreated or treated with fluorinated chemicals (PFAS). Global environmental mandates in California, the EU, and Japan now enforce strict perfluorinated chemical bans. Oasis Jackets offers plant-based, fluorine-free DWR (Durable Water Repellent) wool finishes that repel light rain without compromising natural fabric breathability.
Trend 2: Digital Product Passports (DPP) & NFC Smart Tags
Luxury streetwear brands selling custom varsity jackets above $300 are increasingly embedding encrypted NFC microchips inside chenille patches or neck labels. This enables end-consumers to tap their smartphones to verify authenticity, review supply chain sourcing documents, and track carbon offsets—a key requirement for European compliance by 2026.
Trend 3: Hybrid Material Innovation
Modern urban consumers demand lighter, technical garments. We are seeing rapid growth in hybrid varsity styles: technical 3-layer softshell bodies paired with leather sleeves, or water-resistant ripstop nylon combined with sherpa lining for cold-climate adaptability.
At Oasis Jackets, every production batch passes through an integrated 4-tier Quality Assurance framework, aligned with ISO 9001 and AQL 2.5 (Acceptable Quality Limit) international standard procedures:
Pre-Production Audit
Lab dip & hide shade matching
Inline QC Check
Hourly seam-pull audits
Final Inspection
Metal detection & AQL 2.5
Before bulk production begins, a sealed Pre-Production (PP) Sample is produced and sent to your product development team. Once approved, this sample becomes the single binding benchmark for our factory floor quality auditors. We conduct strict colorfastness to rubbing (AATCC 8 standard), dry-cleaning dimensional stability testing, and seam strength testing to ensure zero sleeve-to-body tear outs.
4. How to Optimize Your Brand’s Sourcing Costs
As a B2B procurement partner, we help clients engineer their tech packs to maximize retail profit margins without sacrificing visual impact:
Consolidate Leather Colorways: Dyeing leather hides in custom colors requires specific tannery minimums. Choosing stock drum-dyed black, off-white, or tan cowhide reduces sleeve costs by up to 18%.
Optimize Chenille Placement: Consolidating back artwork into a single large patch layout reduces embroidery machine run-time (SAM) compared to multiple scattered small badges.
Leverage Multi-Country Production Footprints: Take advantage of our 9 production facilities across Asia and South America to lower duty tariffs under regional trade agreements (GSP, USMCA, EUR.1).
Sleeves: 1.0mm–1.2mm top-grain drum-dyed cowhide, 0.8mm–0.9mm supple lamb nappa leather, or high-flex bio-based PU synthetic leather.
Lining: 100% polyester satin (120 GSM) with 80 GSM diamond quilting or cupro silk alternative.
Ribbing: 2x2 heavy-duty yarn-dyed ribbing with 5% elastane elasticity recovery.
Hardware: Heavy-duty brass snap buttons with customizable painted, polished, or rubberized caps.
What is the minimum order quantity (MOQ) for custom varsity jackets?
Our flexible MOQ framework starts at low minimums per design and colorway for styles utilizing in-stock leather hides and standard wool shades. For fully custom Pantone-dyed wool or custom-tanned leather hues, MOQs are determined by mill minimum dyeing quantities. We work closely with emerging labels to stage initial production runs, allowing sell-through validation before scaling volume orders.
Can you manufacture varsity jackets under my own private label branding?
Yes, 100% private label production is our core operational focus. We handle end-to-end customization, including custom woven neck tags, interior care/content labels compliant with US FTC and EU textile directives, branded brass snaps, embossed leather back patches, custom printed linings, retail hangtags, and branded polybags. Oasis Jackets branding never appears anywhere on your product.
How long does sampling and bulk manufacturing take?
Sample development takes 7–12 business days following tech-pack digitizing and artwork sign-off. Bulk production requires 25–45 days depending on total order units, leather processing schedules, and embroidery patch density. Air freight delivery spans 5–9 days, while ocean freight takes 20–40 days depending on the destination port.
What certifications do your fabrics and factories hold?
Our manufacturing matrix holds comprehensive global certifications, including GRS (Global Recycled Standard), GOTS (Global Organic Textile Standard), OEKO-TEX Standard 100, ISO 9001/14001, amfori BSCI social audit compliance, and Higg Index sustainability ratings. Full transaction certificates (TCs) are provided per order shipment.
How do you ensure the chenille patches do not warp or peel after cleaning?
We stitch chenille loops directly onto 100% heavy wool felt backing with high-density perimeter lock-stitching. The back of each patch is reinforced with a thermo-adhesion film. Prior to sleeve assembly, the patches are heat-sealed and sewn directly into the wool panel, preventing any peeling, warping, or fraying during professional dry cleaning.
Which countries do you ship wholesale orders to?
We ship DDP (Delivered Duty Paid), FOB, or EXW to over 55 countries. Our primary logistics routes serve the United States, Canada, United Kingdom, Germany, France, UAE, Saudi Arabia, Qatar, Australia, and Brazil, with regional sales support desks in 7 key nations.
24/7 Global Sourcing Desk
Ready to Build Your Custom Varsity Jacket Line?
Submit your tech pack, mood board, or garment vector design today. Receive a comprehensive open-costing quote, material swatches, and production timeline within 24 hours.