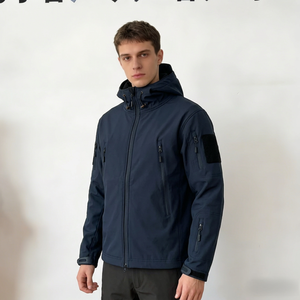
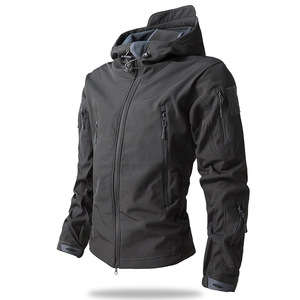
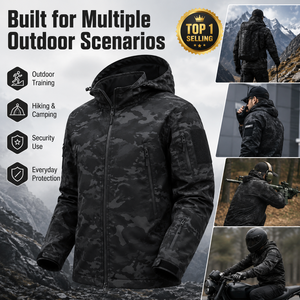
Tactical Outerwear Engineering: Technical Architecture & Material Science Whitepaper
In modern operational environments—ranging from tactical law enforcement interventions to extreme cold-weather survival—the performance threshold of outerwear is non-negotiable. As a top trusted tactical jackets manufacturer and global exporter, our OEM/ODM facilities operate under strict technical frameworks designed to eliminate failure points before garment assembly begins.
1. Advanced Membrane Lamination & Water Column Physics
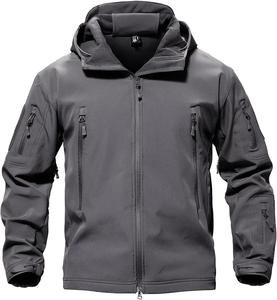
Tactical softshell and hardshell jackets require delicate equilibrium between waterproof protection and sweat vapor evacuation. We utilize advanced 3-Layer (3L) and 2.5-Layer (2.5L) hydrophobic and hydrophilic membrane laminations:
Hydrostatic Head Performance: Ranging from 10,000 mm to 20,000 mm (ISO 811 certified), ensuring zero water penetration even under heavy rain and sustained pressure from tactical backpacks and plate carriers.
Moisture Vapor Transmission Rate (MVTR): Ranging from 10,000 to 18,000 g/m²/24h (ASTM E96 Procedure B), preventing internal condensation build-up during high-exertion operations.
Zero-Degradation Taping: All critical seams are sealed using 13mm to 22mm hot-melt polyurethane (PU) seam sealing tape applied via computer-controlled hot-air welding equipment.
2. Textile Abrasion Resistance & Material Formulation
Tactical shells must withstand continuous friction against concrete, vegetation, and load-bearing gear. Our material portfolio integrates high-tenacity polymers:
Cordura® & High-Tenacity Ripstop Nylon: 300D to 1000D weave densities engineered with cross-hatched reinforcement threads preventing tear propagation.
NIR (Near-Infrared Reflectance) Compliance: Optional dye treatments formulated to absorb or scatter near-infrared radiation, reducing detection signatures under night-vision spectral devices (NVGs).
PFC-Free Durable Water Repellent (DWR): Transitioned to next-generation C0 eco-friendly fluorocarbon-free surface treatments delivering Level 4 spray resistance without persistent bioaccumulative chemicals.
Global Tactical Apparel Sourcing & Industry Development Trends
Data-driven insights into how military gear buyers, law enforcement agencies, and outdoor brands are adapting supply chains for 2025–2030.
Nearshoring & Multi-Country Factory Agility
Global procurement teams are shifting away from single-source manufacturing. By maintaining production networks across 9 countries, enterprise buyers achieve tariff optimization, mitigate geopolitical risk, and secure flexible lead times without compromising audit consistency.
Strict Environmental & Chemical Compliance
Procurement regulations in North America and Europe now mandate GRS (Global Recycled Standard) certified rPET fibers, OEKO-TEX Standard 100 compliance, and complete elimination of PFAS/PFOA fluorocarbons in tactical weather barrier finishes.
Modular Load Integration & Ergonomics
Modern tactical jackets are designed to seamlessly integrate with modular tactical vests, concealed body armor, and communication harnesses. Key trends include low-profile magnetic pocket closures, articulated 3D sleeve patterning, and dynamic underarm ventilation gussets.
As part of a unified global manufacturing organization with over 16 years of technical outerwear excellence, we provide private label clients and institutional distributors with enterprise-grade manufacturing guarantees.
Full Customization from Tech-Pack to Container
From raw sketch or reference sample to final sealed Pre-Production (PP) sample in 7–12 days. We develop custom Pantone fabric dyeing, engineered jacquard linings, silicone brand badges, and specialized hardware pullers.
Rigorous Multi-Tier Quality Assurance (AQL 2.5)
Every production lot undergoes 4-point raw fabric inspection, tensile and tear strength testing, zip-pull endurance testing, in-line stitching symmetry checks, and 100% needle detection before final carton sealing.
Our client portfolio spans global institutions, private label streetwear brands, government supply contractors, and tactical outfitters across 55+ countries. With administrative and design desks in the USA, UK, UAE, Australia, Germany, France, Saudi Arabia, Brazil, and Qatar, we provide local account management coupled with factory-direct pricing economics.
Tactical Jacket Procurement & Manufacturing FAQ
Technical guidance and answers for wholesale buyers, product managers, and procurement officers.
What is the minimum order quantity (MOQ) for custom tactical jacket manufacturing?
Our Minimum Order Quantity (MOQ) is structured flexibly to support both growing brands and high-volume institutional procurement. For styles utilizing our certified in-stock tactical fabrics (such as 3L softshell or high-density micro-ripstop), MOQs start low per style and colorway. For fully customized mill-dyed fabrics, unique camouflage prints, or bespoke hardware development, MOQs are governed by fabric mill minimums. Contact our team to request a tailored MOQ calculation based on your tech pack.
What fabric specifications and membrane options do you recommend for tactical use?
Fabric selection depends heavily on the intended operational environment:
All-Weather Softshell: 92% Polyester / 8% Spandex or 100% Nylon outer shell bonded to a TPU membrane (10K/10K) and 50D micro-fleece backing.
Extreme Rain & Cold Shells: 3-Layer 100% Ripstop Nylon with PTFE or TPU lamination (20,000mm hydrostatic head, fully seam-sealed).
Winter Combat Padding: 20D/40D Down-proof ripstop shell insulated with 100–200 GSM GRS-certified recycled synthetic polyfill or IDFL-certified down.
Can you manufacture tactical jackets with custom branding and private label trim?
Yes. Private label manufacturing is our core specialty. We handle complete brand execution including custom woven neck labels, care and content labels compliant with US FTC and EU textile directives, rubber/silicone sleeve patches, velcro loop panel placements, branded zipper pullers, custom lining prints, and branded shipping boxes. No supplier branding appears on your finished garments.
What is the standard timeline for sampling and bulk production?
Our standard production workflow operates on the following timeline:
Proto & Fit Sampling: 7 to 12 working days following tech pack approval and raw material staging.
Pre-Production (PP) Sample Approval: 5 to 7 days for physical delivery and sign-off.
Bulk Manufacturing: 25 to 45 days depending on total order volume, trim complexity, and factory scheduling.
Global Shipping: Air freight (5–9 days) or Sea freight (20–40 days DDP/FOB/EXW).
What compliance certificates and factory audit standards do you maintain?
Our manufacturing facilities and raw material partners maintain full compliance with international standards, including ISO 9001 quality management, OEKO-TEX Standard 100 chemical safety, Global Recycled Standard (GRS), BSCI social compliance, and Higg Index environmental impact tracking. Transaction certificates are provided per shipment upon request.
How do you ensure consistency across large volume orders?
Every order is checked against a physically sealed Pre-Production (PP) sample. Our QA team utilizes standardized AQL 2.5 inline inspection protocols covering stitch tension, seam strength, zipper smoothness, color shade consistency (under D65 light booths), and dimensional stability after wash testing.
Partner with a World-Class Tactical Jacket Manufacturer
Looking for factory-direct OEM/ODM pricing, certified technical fabrics, and reliable global delivery? Speak with our senior outerwear merchandising desk today.