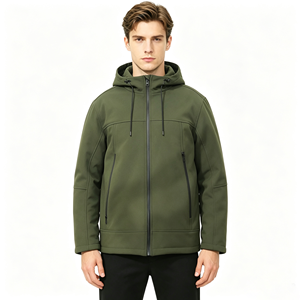
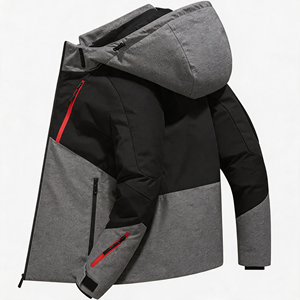
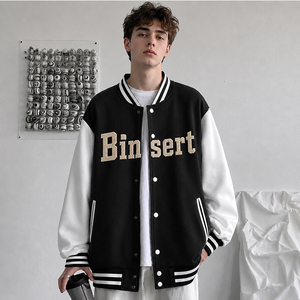
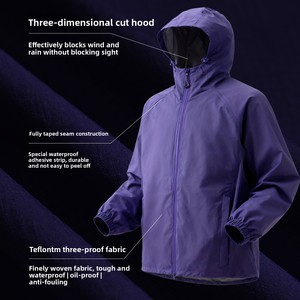
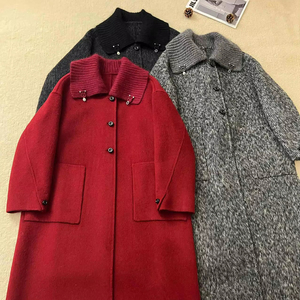
Explore our primary outerwear manufacturing blocks. Each style is fully customizable across fabric density, colorways, insulation metrics, surface branding, and hardware trims.
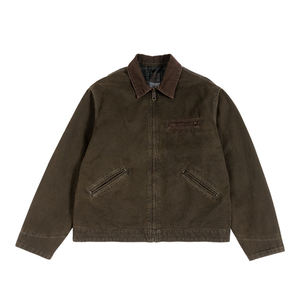
14 oz heavy cotton canvas teamwear coat featuring direct chenille chest embroidery, enzyme vintage washing, and diamond quilted satin lining.
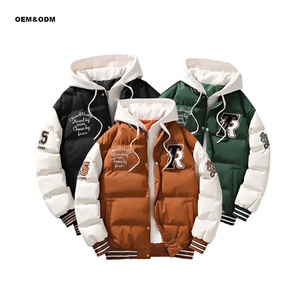
High-density matte nylon shell combined with warm synthetic insulation, contrast athletic sleeve striping, and a detachable fleece-lined hood.
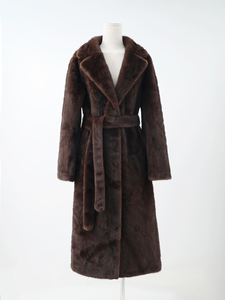
Ultra-soft plush pile faux fur overcoat designed for premium corporate hospitality teamwear, featuring concealed snap enclosures and custom belted waist.
10,000mm hydrostatic head waterproof 3-layer laminated shell bonded with 300 GSM thermal polar fleece lining for alpine staff and winter teamwear.
Recycled post-consumer canvas fabric finished with fluorine-free DWR coating, storm-flap enclosure, and detachable ergonomic hood.
Authentic 24 oz Melton wool body paired with full-grain leather sleeves, high-density 3D chenille club patch work, and yarn-dyed rib cuffs.
Sleek matte-finish membrane jacket with invisible pocket construction, laser-cut ventilation ports, and subtle tone-on-tone brand execution.
Double-breasted wool blend structure engineered for staff, team delegation, and corporate travel, offering superior drape and pill resistance.
As a tier-one OEM teamwear jackets supplier and global exporter, our vertically integrated infrastructure spans multiple manufacturing hubs worldwide to ensure competitive tariffs, rapid turnarounds, and rigorous compliance.
Every single batch undergoes rigorous four-point fabric inspection, seam pull-strength testing, metal detection, and pre-shipment AQL 2.5 quality control before leaving our dock.
We maintain full traceability with GRS (Global Recycled Standard), OEKO-TEX Standard 100, GOTS organic cotton, and IDFL certified responsibly harvested down insulation.
Full-service export handling including custom clearing, tariff optimization, air freight express sample dispatch, and sea freight consolidation under DDP, FOB, or EXW terms.
How international sports brands, collegiate athletic departments, and corporate uniform buyers are restructuring their jacket supply chains for flexibility, compliance, and speed.
Global buyers are shying away from massive inventory blockages. Modern OEM procurement requires suppliers capable of starting low initial MOQs (minimum order quantities) per style while offering rapid CAD-patterning and 7-day proto turnaround to test regional market demand.
3D visual rendering and computerized pattern grading (such as Lectra and Optitex) are replacing manual tech pack reviews. This cuts proto cycle errors by 45% and allows teamwear managers to verify sleeve drop, ribbing tension, and logo scale virtually.
Corporate ESG policies now require verifiable sustainability. Procurement contracts heavily favor OEM suppliers utilizing post-consumer rPET shells, PFC-free DWR coatings, and biodegradable lining textiles accompanied by valid GRS Transaction Certificates (TCs).
The global teamwear market is undergoing a seismic shift toward multi-country manufacturing resilience. Brands can no longer rely on single-origin production due to fluctuating import tariffs, shipping bottleneck risks, and localized cost inflation. Leading custom OEM teamwear jacket suppliers are establishing distributed manufacturing networks across South Asia, Southeast Asia, and East Asia.
By balancing fabric mill proximity with specialized assembly lines (such as dedicated down-injection rooms or specialized taped-seam machinery), top exporters ensure consistent unit economics, robust contingency capacity, and compliance with stringent labor standards demanded by major sports leagues and corporate clients.
An engineering benchmark of modern technical outerwear fabrics, membrane lamination, and specialized decoration techniques used in custom teamwear manufacturing.
| Outerwear Category | Shell Fabric Weight & Spec | Membrane / DWR Rating | Insulation & Lining | Recommended Teamwear Decoration |
|---|---|---|---|---|
| Pro Sideline Parka | 210T Ripstop Nylon / 75D Poly | 15,000mm H₂O / 10,000g MVTR | 200 GSM Recycled Polyfill | 3D Molded Silicone Badges + Waterproof Zippers |
| Collegiate Varsity Jacket | 24oz Melton Wool / Grain Leather | C0 Eco-DWR (Sleeves) | Quilted Polyester Satin (120 GSM) | Heavy Chenille Embroidery + Yarn-Dyed Ribbing |
| Technical Ski & Snow Shell | 3-Layer Laminated Polyester | 20,000mm Waterproof / Full Tape | 300 GSM Anti-Pill Polar Fleece | Reflective Heat Transfer + Laser-Cut Vents |
| Vintage Streetwear Bomber | 12oz–14oz Heavy Cotton Canvas | Enzyme / Stone Wash Finish | Taffeta with Lightweight Scrim | Direct Chain-Stitching + Embossed Leather Patch |
| Executive Travel Overcoat | 650 GSM Australian Wool Blend | Hydrophobic Anti-Stain Coating | Bemberg / Viscose Jacquard | Laser-Etched Buttons + Subtle Tone Woven Label |
Modern team jackets utilize 2.5-layer and 3-layer thermal TPU membranes. By bonding a micro-porous membrane directly between the abrasion-resistant outer shell and inner lining, garments achieve 10,000mm to 20,000mm hydrostatic head protection without adding bulk or sacrificing athlete mobility during sideline performance.
Engineered teamwear now incorporates localized thermal insulation zones. By placing high-loft down or synthetic polyfill across core chest areas while inserting breathable 4-way stretch softshell panels under arms and down back channels, jackets deliver dynamic climate control during intense warm-ups and cold sideline rest periods.
Standard screen printing is rapidly being replaced by multi-texture branding options. OEM teamwear suppliers now combine 3D chenille patches, high-frequency raised silicone logos, laser-etched metal hardware pullers, and reflective high-visibility thermal transfers that withstand repeated commercial industrial laundering.
Direct technical answers to common questions asked by apparel sourcing managers, importers, and sports team buyers.
Our baseline OEM minimum order quantity (MOQ) typically starts at 100 to 300 pieces per style/colorway for stock-fabric programs with custom embroidery, printing, and branded trims. For fully custom mill-dyed shell fabrics, bespoke jacquard linings, or specialized technical membranes, factory mill minimums may require 500 to 1,000 pieces. We also offer low-volume starter programs for emerging private label brands looking to test new product lines.
Our standard manufacturing timelines are broken down into distinct milestone phases:
Yes. Private label manufacturing is our core enterprise service. We manufacture completely white-label garments with your brand's specifications. This includes woven neck labels, care/content labels compliant with US FTC and EU textile regulations, customized branded zipper pulls, embossed leather or rubber patches, printed polybags, custom hangtags, and branded shipping cartons. Zero supplier branding appears on your finished goods.
We provide full lab documentation per production lot. Our fabric certified options include GRS (Global Recycled Standard) for recycled polyester and nylon shells, OEKO-TEX Standard 100 verifying toxic-substance-free dyes, GOTS for organic cotton elements, ISO 9001 factory quality audits, and IDFL certification for ethically harvested down insulation. Third-party testing by SGS, Intertek, or Bureau Veritas can be arranged prior to shipment.
To provide an exact FOB or DDP unit quotation, our merchandising team requires a basic 2D vector flat sketch, CAD file, or a reference garment photograph along with your target fabric specification (or intended weather use case), estimated quantity breakdown per size, and desired decoration methods (e.g., embroidery, screen print, silicone badge). If you do not have a formal tech pack, our in-house apparel technicians can create one for you.
We support all primary international trade terms including DDP (Delivered Duty Paid), FOB (Free On Board), and EXW (Ex Works). Under DDP terms, our global export division handles all customs documentation, import duties, harbor clearance fees, and final truck delivery directly to your central warehouse in the US, UK, Canada, Australia, EU, or GCC regions.
Our factory quality management system implements a 4-tier prevention protocol: 1) Roll-by-roll fabric 4-point visual inspection and shade matching before cutting; 2) Trim pull-strength testing (zipper teeth, snap buttons, drawcords); 3) Inline hourly sewing audits for seam alignment and insulation density; and 4) Final pre-pack AQL 2.5 random sampling inspection with metal detection scanning.
Connect directly with our senior outerwear merchandisers and engineering team. Get a detailed technical cost breakdown, fabric lab-dip proposals, and production timelines within 24 hours.